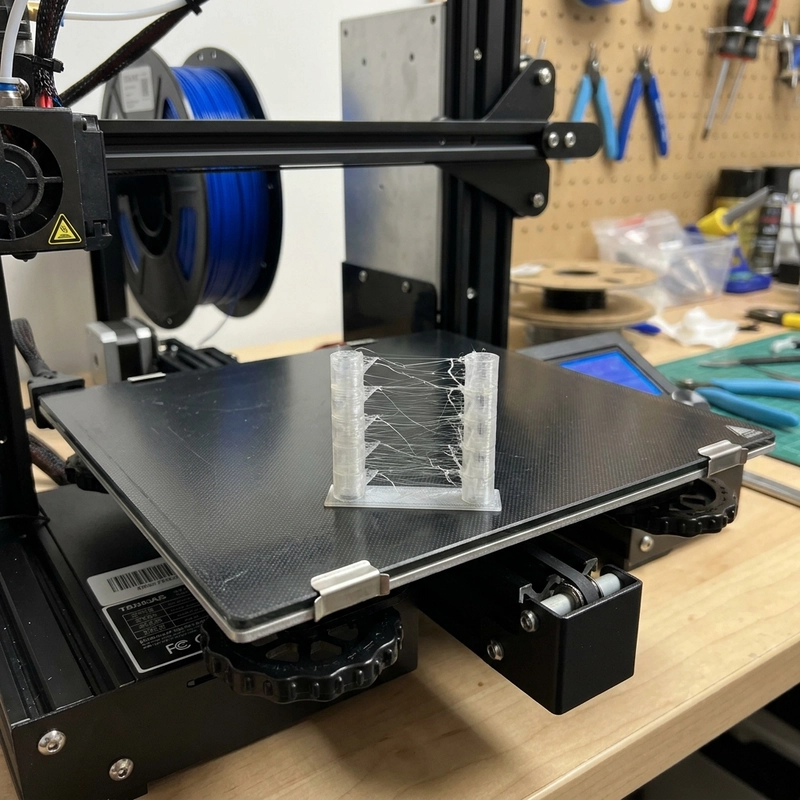
FDM stringing appears as fine plastic threads between features when material oozes during travel. Temperature, retraction, travel behavior and filament condition can interact. Start with the approved printer-material profile, check for contamination or moisture, and change one setting at a time. Record the comparison so a cleaner test print can be checked against the final part requirements.
Why Plastic Leaks During Travel Moves
When the printer finishes one extrusion segment and moves the nozzle to another, pressure remains inside the hotend melt zone. If the nozzle is hot and the filament is fluid, a small amount can ooze out during the travel move. Retraction pulls filament back to relieve that pressure. Travel speed determines how long the nozzle spends in motion with residual melt exposed. Temperature controls viscosity—hotter filament flows more easily. Moisture adds steam bubbles inside the melt zone that push material out unpredictably, making stringing worse and less consistent. Four variables interact: retraction distance and speed, nozzle temperature, travel speed and filament dryness.
Bowden and direct-drive systems can require different retraction settings, but there is no universal distance range for either type. Begin with the equipment’s material preset and respect its limits. Flexible filament can stretch or feed inconsistently during retraction, so validate both stringing and reliable extrusion.
| Adjustment | Effect | Risk If Overdone |
|---|---|---|
| Retraction distance | Relieves nozzle pressure during travel | Filament grinding, clogs or gaps at extrusion restart |
| Retraction speed | Controls how quickly pressure is relieved | Filament stripping or extruder motor skipped steps |
| Nozzle temperature | Lower temperature reduces melt fluidity and oozing | Weak layer adhesion or under-extrusion |
| Travel speed | Less time for leakage between features | Ringing, ghosting or skipped steps if exceeding motion limits |
| Filament drying | Eliminates steam-driven oozing | Material degradation if dried above recommended temperature |
Retraction Calibration for FDM Stringing
Use a small repeatable test part and retain the original profile. Make controlled changes within the equipment limits, checking both strings and extrusion restart gaps. Prusa’s stringing guidance recommends factory presets and explains how excessive retraction speed can cause skipped steps. Do not add restart compensation automatically without checking the result.
If the extruder clicks after many retractions during a detailed print, heat creep or filament grinding may be starting. Slicer settings like maximum retraction count and minimum extrusion distance window prevent the extruder from retracting the same section of filament repeatedly, which can grind a flat spot into the filament and cause feed failure. Combing, wipe and coasting settings can reduce stringing on cosmetic surfaces, but they should not be used to hide a wet filament or excessive temperature problem. For visible surfaces, I set travel moves to avoid crossing perimeters whenever possible—internal travel marks may be acceptable while scars across the front face are not.
Temperature and Drying: Fix the Material Before the Slicer
Popping or bubbles warrant checking moisture before extensive slicer changes. Use the exact filament and spool instructions; published drying schedules vary by formulation and equipment. Then compare temperature settings without sacrificing layer bonding. Mechanical cleanup may suit fine strings, but heat can deform a part and must not be described as harmless to every geometry.
Material-Specific FDM Stringing Behavior
Treat PLA, PETG, TPU, nylon and filled blends as separate material profiles rather than assigning one temperature or retraction recipe to each family. Use the exact grade’s processing guidance and a repeatable test. For flexible filament, confirm feeding as well as retraction; for filled material, check nozzle compatibility and wear. Compare the finished part against the agreed surface requirement.
For appearance prototypes, review travel paths across cosmetic surfaces before relying on cleanup. Fine strings may be removable, but sanding or heat can change detail and dimensions. Trial any finishing method on a representative sample and inspect the visible face afterward.
For batch production, stringing should be judged with the final material batch and production nozzle, not only with a calibration spool. Pigments, fillers and flexible blends change melt behavior enough to shift the stringing threshold. Record the tuned temperature, retraction distance, retraction speed, travel speed and drying condition. If any of those variables change, rerun a small stringing tower before starting a full build plate.
Practical Fix Order for FDM Stringing
- Dry the filament if moisture is suspected—popping sounds or rough extrusion are clear indicators.
- Print a temperature tower and choose the lowest stable range that still produces good layer adhesion.
- Calibrate retraction distance and speed on a small stringing test tower; adjust one parameter at a time.
- Review travel speed within the approved machine profile and stable motion limits; check surface quality and feeding after a change.
- Enable wipe, combing or avoid-crossing-perimeters settings for cosmetic surfaces if fine strings persist.
- Check for heat creep if stringing worsens during long prints—a degrading hotend fan or clogged heatsink fins can gradually raise melt zone temperature.
FDM stringing should be evaluated with the final material and production setup. Keep the validated profile and conditioning record, and recheck affected settings when the nozzle, material or machine changes. Zesmir project review can clarify the required surface finish; it is not a guarantee that every print will be string-free.
Need FDM prints with a defined cosmetic finish? Contact Zesmir with the file, material and visible-surface requirements so the proposed route and acceptance criteria can be reviewed before quoting.