Resin print paint adhesion is easy to blame on the paint, but the paint is often only the last part of the mistake. Support scars, uncured residue, sanding dust, glossy cured skin, and a rushed primer layer can all make a coating peel even when the print itself looks fine. I treat resin print paint adhesion as a surface-preparation problem before I treat it as a coating-brand problem.
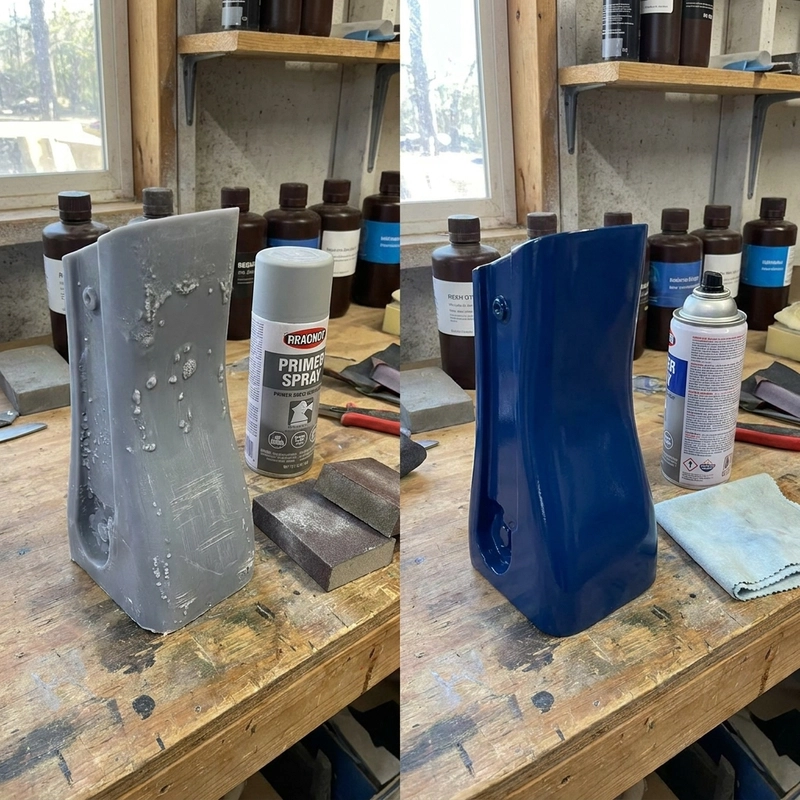
The ugly part is that adhesion problems may not show up right after spraying. A sample can look acceptable on the bench, then chip around support marks during packing, handling, or clear coating. The coating fails at the weak interface. That weak interface may be uncured resin, trapped alcohol, skin oil, polishing compound, or simply a sanding scratch pattern that is too smooth for the primer to bite.
Resin print paint adhesion starts before primer
After printing, remove uncured residue using the wash method specified for the resin, then dry and post-cure as required. Cavities and trapped solvent need particular attention. Do not apply primer over residue or use a clean-looking outside surface as evidence that every pocket is clean.
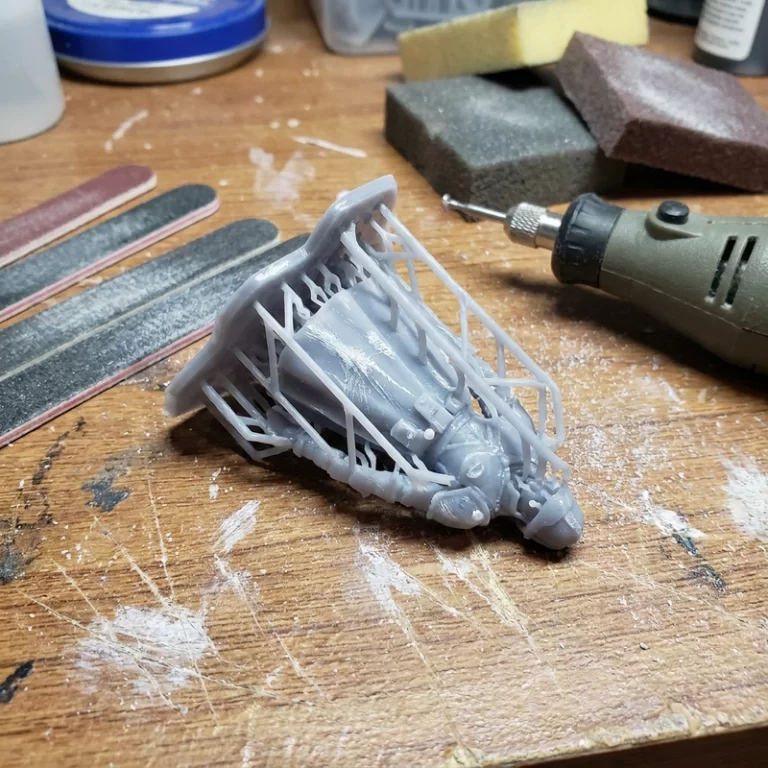
Do not sand a resin part while it still carries uncured residue. Complete the required processing first, then level support marks using a sanding sequence compatible with the resin and coating. Avoid erasing detail or polishing the surface beyond the primer’s preparation requirements. Control sanding dust and use the protection specified by the material and coating safety data sheets.
Support removal is a coating issue too. If a heavy contact is torn off, it can leave a crater with damaged resin around it. That spot may need local filling, sanding, and primer surfacer, not just color paint. For support placement and contact design, the related Zesmir article on 3D printing support design is worth reading before the next print is prepared.
Primer choices for resin print paint adhesion
A primer has two jobs: bonding to the resin and giving the color coat a consistent surface. Thick primer is not a repair plan. Burying residue or deep support gouges can leave a weak coating stack. Follow the primer and paint system’s specified coat thickness and recoat conditions, using a test piece before finishing a visible model.
Spray setup depends on the coating, thinner, nozzle and application equipment. Too close or too wet can flood details; dry spray can leave a rough surface with poor leveling. Use the coating system’s application guidance and spray a scrap print or hidden area before a visible face on a figurine, product model or display part.
Drying time depends on the coating system, film thickness and environment. Follow the product’s recoat, handling and full-cure requirements. “Dry to touch” is not the same as ready for masking tape, clear coat, packing foam or assembly pressure.
Checking resin print paint adhesion after sanding
Before painting, I check the surface under low-angle light. That light shows support scars, sanding waves, and glossy patches better than overhead light. If a shiny island remains in the middle of a matte sanded area, the primer will read it too. I also wipe the part with a suitable cleaner and let it flash off fully. Do not trap solvent under primer.
Masking is another small adhesion check. If tape pulls color off a corner, examine the tape type, adhesive strength, dwell time and removal method as well as contamination, cure and coating thickness. Test the complete coating-and-tape combination on a hidden tab or underside before masking a visible face.
Adhesion testing should be scaled to the part risk. A display-only figurine may only need handling and tape checks on a hidden area. A product prototype that will be assembled and disassembled may need more aggressive testing. Do not claim a coating is production-qualified without the actual test method and acceptance criteria. The NIST surface metrology resources are useful background when surface texture and measurement language need to be kept precise.
Support marks, clear coat, and batch consistency
Clear coat can save a finish, but it can also expose bad preparation. A hot clear can attack weak color coats. A heavy gloss clear can pool around small details. A matte clear can make uneven sanding more visible. I like approving one complete stack: resin, cure, sanding grit, primer, color, clear, drying time, and packing method. Changing one layer changes the whole stack.
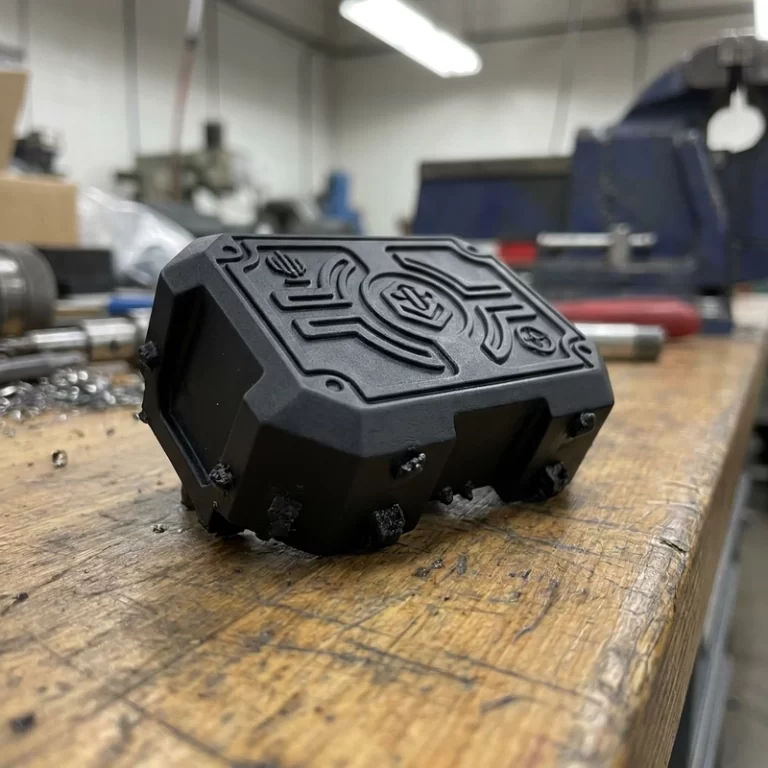
For black or dark resin parts, color inspection is trickier because scratches and dust show quickly. The Zesmir article on black SLA resin 3D printing goes deeper into matte surface and detail visibility. If the paint is meant to hide layer texture instead of only adding color, also compare against the 3D printing surface roughness article before choosing the process.
The safest RFQ note is simple: tell the supplier which faces are cosmetic, whether support marks are allowed, what coating level is expected, and whether the finished part will be handled, shipped individually, or packed in bulk. Resin print paint adhesion improves when the print plan, support plan, and coating plan are treated as one workflow.