Engineering plastic 3D printing material selection should start with the job the part must survive, not with a material name that sounds strong. A request for "ABS or nylon" is incomplete without temperature, load, chemical exposure, assembly method and surface requirements. Establish those use conditions first, then choose the process and grade.
The same plastic family can behave differently in FDM, SLS, MJF, or high-temperature extrusion. Moisture, orientation, infill, annealing, chamber temperature, and post-processing all move the final result. A datasheet is a starting point. A printed part is still a printed structure with layer direction, surface roughness, and process history.
Engineering plastic 3D printing material selection by failure mode
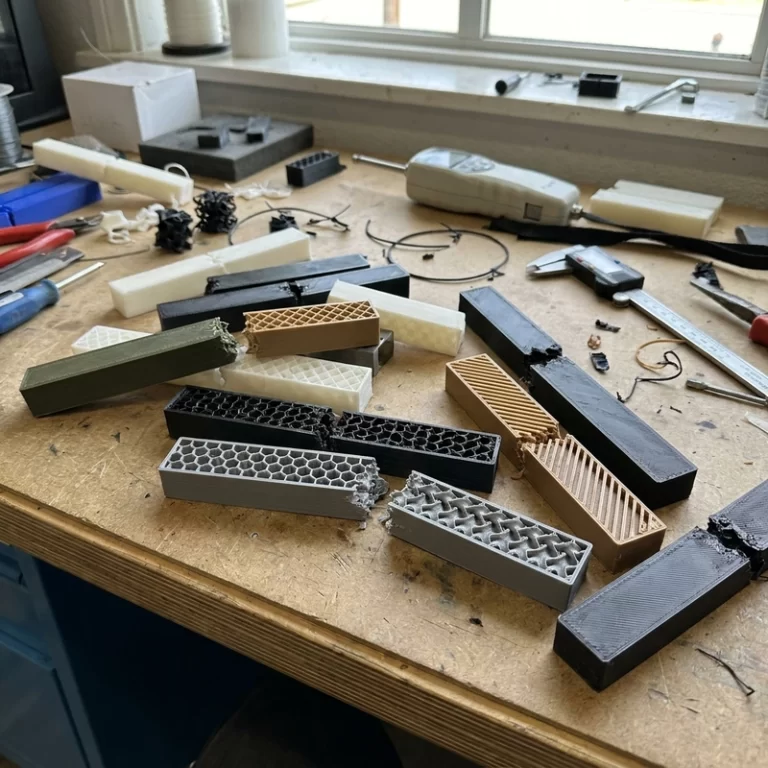
I like asking what failure would be unacceptable. If the part softens near a motor, heat resistance matters. If screw bosses crack, impact and notch behavior matter. If clips must flex, elongation and fatigue matter. If the part sits near oil, coolant, alcohol, or cleaning fluid, chemical resistance matters. If it is only a shape model for a meeting, a cheaper material may be enough.
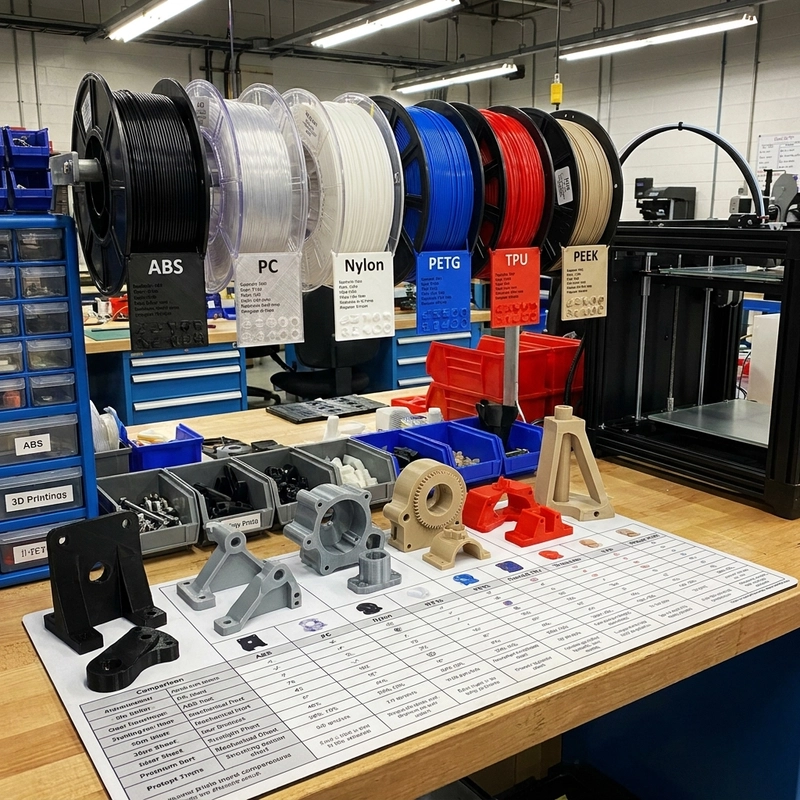
ABS is often a candidate for sanded and painted housings or appearance prototypes. Compare the proposed filament grade and printed-condition properties rather than assigning one tensile strength or heat-deflection temperature to all ABS. Use the material supplier’s profile within the printer’s approved temperature limits, and assess enclosure control and warping for the actual geometry.
PC and PC blends can be candidates when heat resistance and toughness matter, but their processing and properties depend on formulation. Confirm the exact grade, drying requirements and approved printer profile. Prusa’s filament material guide separates material-specific hardware and temperature requirements; a setting for one PC blend is not a specification for every polycarbonate print.
Nylon, PETG, TPU, and high-temperature plastics
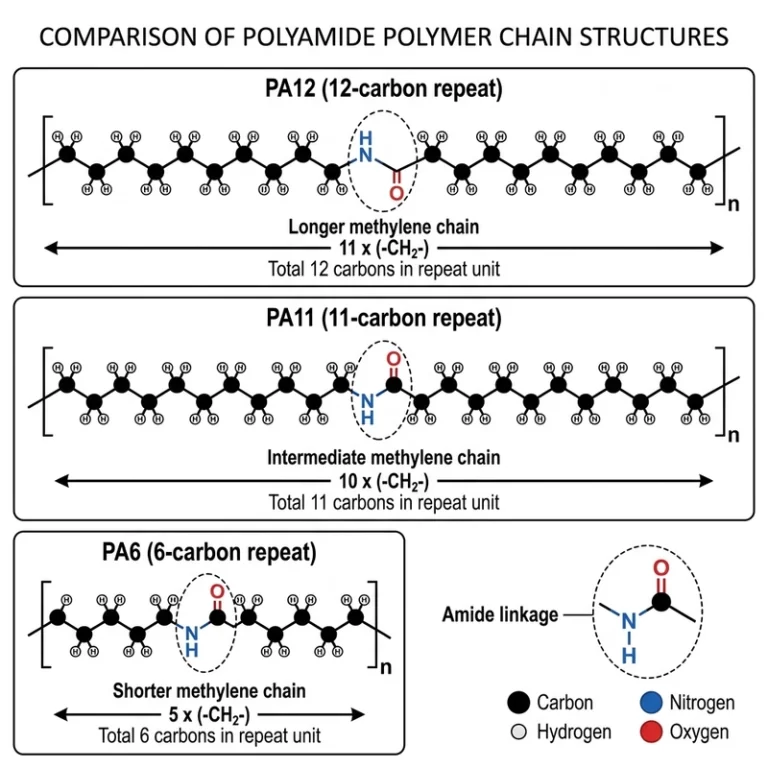
Nylon is a good answer for many functional parts, especially fixtures, brackets, snap features, and wear-prone components. It is not a carefree answer. Nylon absorbs moisture. Wet nylon can print with bubbles, rough surface, weak layers, and inconsistent dimensions. If nylon is selected, drying and storage should be part of the quote. The Zesmir article on nylon 3D printing moisture control goes deeper into that problem.
PETG can be a practical option for covers, brackets and functional prototypes, although stringing and small-feature definition still need attention. TPU is a candidate for flexible grips, bumpers and protective parts. Specify the actual grade and Shore hardness: wall geometry and infill also change the feel, so the polymer name or hardness alone does not predict the finished response.
PEEK, PEI, and other high-temperature plastics are not just expensive versions of PC. They need high nozzle temperature, hot chamber control, drying, and careful design. They make sense only when the use condition justifies the process difficulty. For many prototypes, a lower-cost engineering plastic plus design validation is the better first step.
Engineering plastic 3D printing material selection and process choice
Material selection cannot be separated from process selection. FDM can be economical for large prototypes and fixtures, but layer direction and visible bead lines matter. SLS and MJF offer powder-supported geometry and nested nylon batches, with texture, cleaning and fit constraints of their own. SLA offers detail and appearance options; compare the exact cured resin with the required load rather than assuming that every resin is either structural or fragile.
In practical RFQ work, I also check whether the part will be post-processed. Sanding and painting push the choice toward ABS or resin in some appearance projects. Heat-set inserts, tapping, and repeated screw assembly push the choice toward nylon, PC, or a reinforced grade. Outdoor use raises UV and water questions. None of those details are glamorous, but they decide whether engineering plastic 3D printing material selection holds up after the sample leaves the printer.
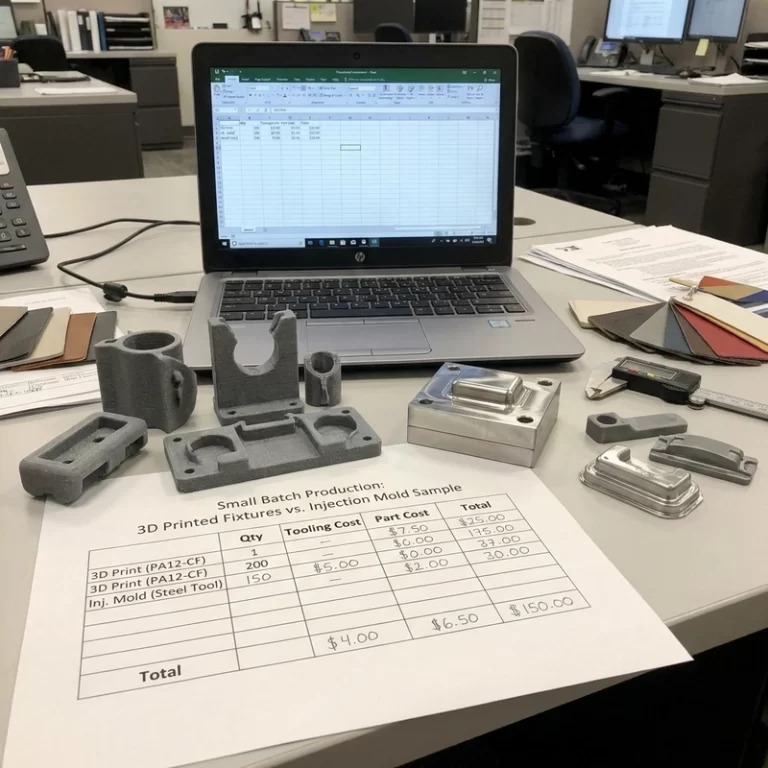
Batch consistency belongs in the same discussion. A one-off prototype can tolerate more hand correction than a repeat batch of fixtures or housings, so the selected plastic should match the expected production rhythm.
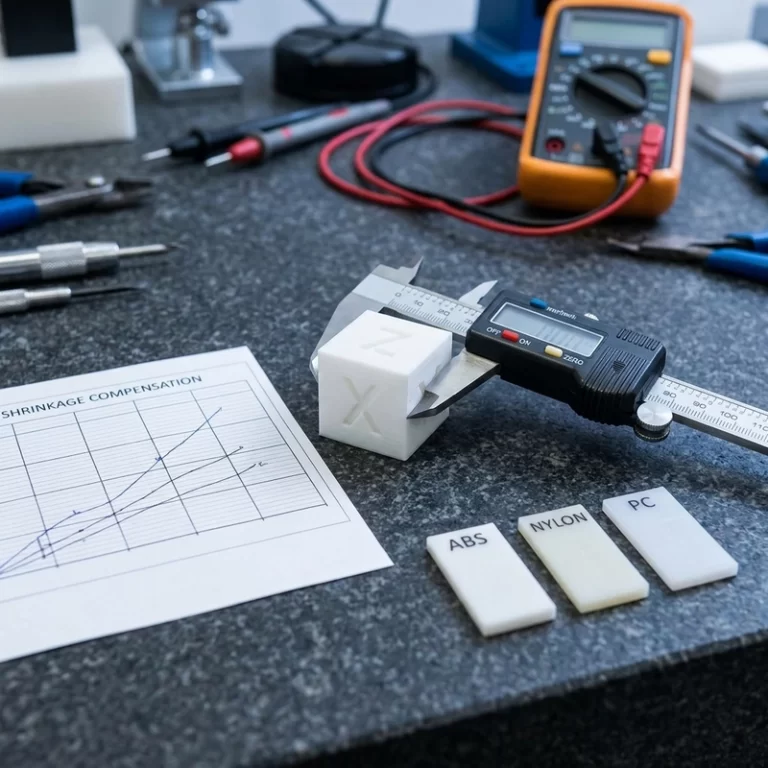
Accuracy also changes the decision. If a part has tight holes, mating faces, and assembly datums, read the related Zesmir article on engineering plastic 3D printing dimensional accuracy before choosing the material. A strong material printed with poor compensation can still fail the assembly.
For general additive manufacturing terminology, ISO/ASTM 52900 is a useful reference point. It helps keep process names clear when comparing extrusion, vat photopolymerization, and powder-bed fusion routes.
A short material decision table
| Need | Common starting option | Check before ordering |
|---|---|---|
| Painted enclosure prototype | ABS or resin, depending on detail | Warping, sanding, primer, cosmetic faces |
| Functional fixture | Nylon, PETG, PC, or filled nylon | Load direction, heat, thread inserts, wear |
| Heat near motor or lamp | PC, high-temp nylon, PEI/PEEK when justified | Real temperature and chamber capability |
| Flexible bumper or soft grip | TPU | Shore hardness, wall thickness, support removal |
| Low-cost large prototype | PETG, ABS, or PLA for non-heat use | Size, distortion, finish, assembly |
My RFQ note for engineering plastic 3D printing material selection is simple: list the use temperature, load direction, chemical exposure, surface finish, quantity, and which dimensions must fit. Without those details, the material choice becomes a guess. With them, the cheapest acceptable material is often easier to find than the strongest-sounding one.