Wood-filled 3D printing materials are polymer composites, not printable lumber. Most printable grades mix wood powder, sawdust or fiber with a binder such as PLA. The part may smell warm, sand differently and show a matte wood-like surface, but its strength, heat limit and printability still come from fiber size, fiber ratio, binder behavior, moisture and nozzle control.
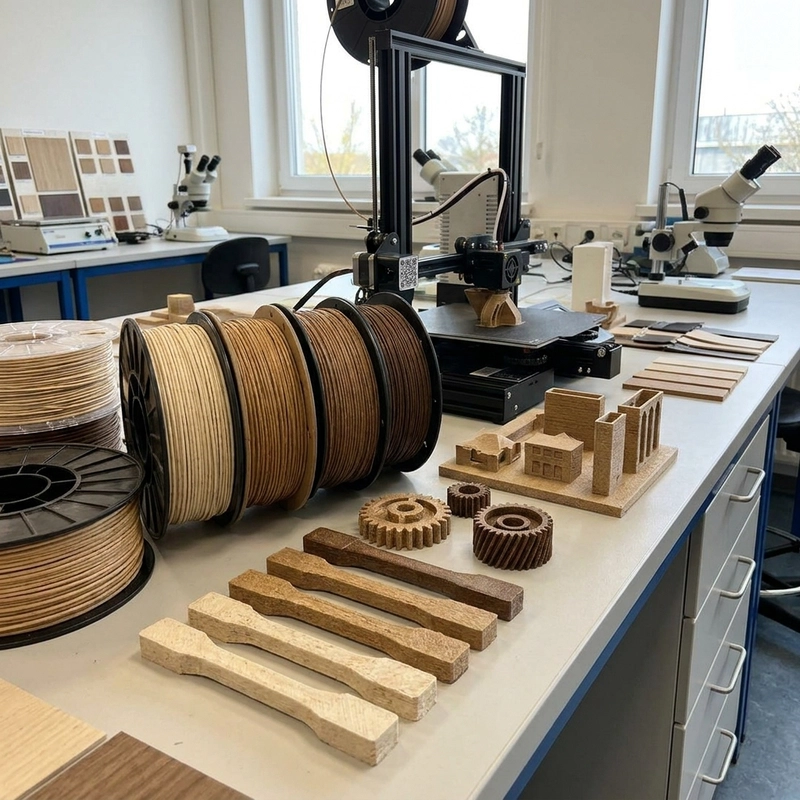
I like these materials for architectural models, cultural products, display props, educational samples, low-load product mockups and decorative prototypes. I do not treat them as structural wood or engineering plastic. The higher the wood content, the more the material may look natural, but printability can get worse quickly.
Wood-Filled 3D Printing Materials Depend on Fiber Size
Wood-filled printing materials use processed wood particles or fibers sized for a particular formulation and feed system. The dimensions of fibers in natural softwood or hardwood do not directly specify what can pass through a filament-printing nozzle. Check the actual filler distribution, dispersion and material supplier’s nozzle guidance.
For filament printing, large particles, poor dispersion and moisture can disrupt feeding or clog the hot end. Choose nozzle size and material using the filament supplier’s guidance. Wood-filled filament should not automatically be assigned the same abrasion requirement as carbon-fiber or metal-filled filament; the formulation matters. A larger nozzle may trade fine detail for more reliable flow.
For base polymer behavior, compare with PLA 3D printing strength. For broader composite material selection, see engineering plastic 3D printing material selection.
Fiber Ratio Is Not the Whole Story
Adding more wood filler does not guarantee higher printed strength. The outcome depends on the matrix, filler distribution, interface bonding, voids and print direction. Excess filler can reduce extrusion consistency and layer bonding. Compare specimens from the actual printable formulation rather than extrapolating a fixed strength increase from filler percentage.
For a decorative model, choose a printable grade by its surface appearance, detail and finishing behavior. A furniture-like or load-bearing experiment needs a separate mechanical assessment of the formulation and printed geometry. The highest wood fraction on a formulation sheet is not necessarily the most reliable or strongest printed part.
Color and texture also move with processing. Higher nozzle temperature or slower speed can darken some wood-filled filaments, which may be useful for a warmer tone but risky for repeat color matching. Sanding exposes fiber differently from the as-printed surface. Stain may take unevenly because the part is still a polymer composite. For a batch of display products, I would approve a finish sample before printing a full set.
Binder Behavior in Wood-Filled 3D Printing Materials
The matrix largely controls processing and service limits. A PLA-based wood filament should not inherit a single heat rating from the name PLA; check the grade and any thermal treatment. Gypsum, cement, starch-based and epoxy-bound wood composites are different material systems, not interchangeable filament recipes. A natural ingredient alone does not establish lower environmental impact or recyclability.
Wood filler and polymer do not automatically form a strong interface. Surface treatments and coupling agents can change bonding, but their benefit depends on formulation and processing and may come with other tradeoffs. Use results from the actual material and printed test specimens; an improvement reported for a different composite does not establish the strength of this part.
Toughening additives need the same caution. A small TPU phase can improve impact behavior in some wood-plastic blends, but it may reduce stiffness, change extrusion pressure and make edges feel softer. Epoxy or inorganic binders may improve certain properties while adding curing, brittleness or post-processing limits. The best binder is the one that matches the part’s load, heat, finish and manufacturing route, not the one with the longest material description.
Printability, Moisture and Finish
Wood fiber holds moisture. Wet material can bubble, roughen the surface and weaken layers. Dry the filament according to supplier guidance and store it sealed. Slow the print enough for the composite to flow. Use retraction carefully because fiber friction can make pressure less predictable. Nozzle temperature should be high enough for smooth extrusion but not so high that the wood phase darkens or degrades.
Nozzle choice is not a small detail. A brass nozzle may work for a short decorative test, but filled materials can wear it and change the opening over time. A worn nozzle changes line width, surface texture and dimensions. If the model has tiny holes, sharp text or thin pins, the wood-filled grade may be the wrong material even when the color is perfect. Sometimes it is cleaner to print plain PLA or resin and apply a wood-like finish afterward.
For wood-filled 3D printing materials, the RFQ note should include desired texture, color tolerance, finish method, minimum feature size, heat exposure and whether the part is decorative or load-bearing. Those details matter more than asking for the highest fiber percentage.
These materials can sand, stain or paint nicely when the formulation matches the finish. They are useful for texture, warmth and appearance. They are not a replacement for machined wood or structural composite laminate. The NIST additive manufacturing page is useful process background, but the material decision still comes down to the part’s size, fiber texture, nozzle risk, heat exposure, finish and load. Wood-filled 3D printing materials work best when the buyer wants a controlled wood-like composite, not a fantasy version of real wood.