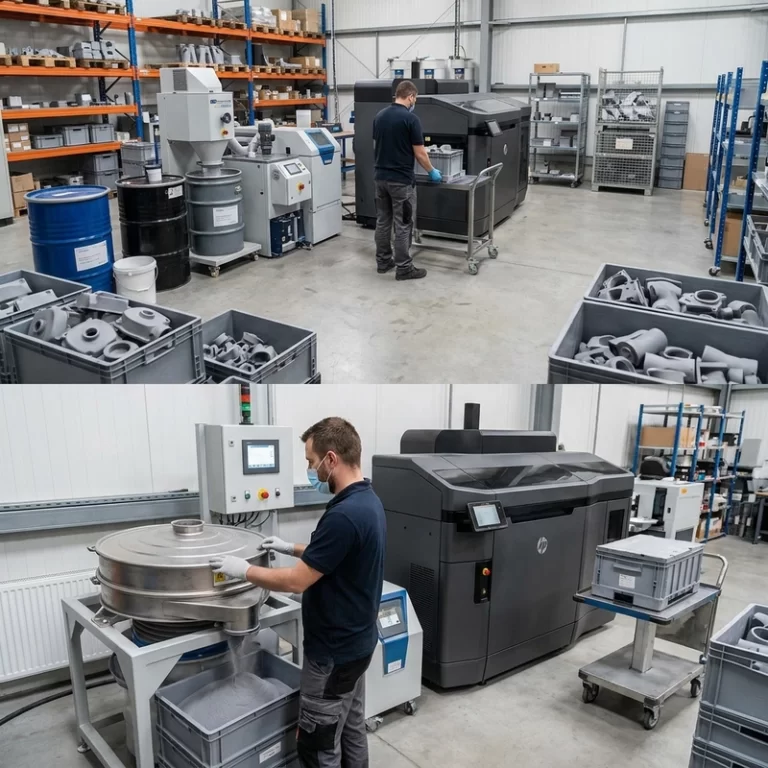
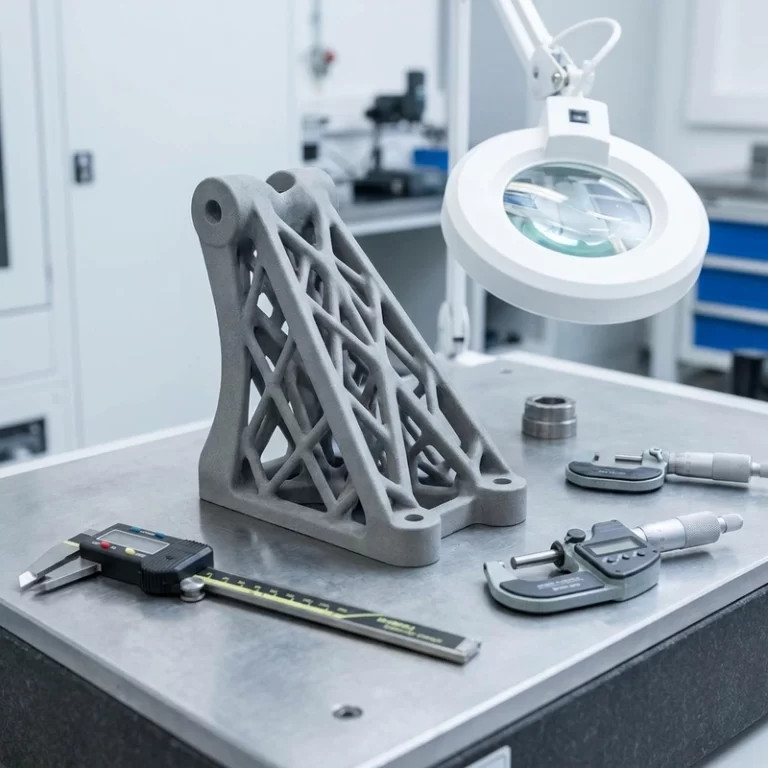
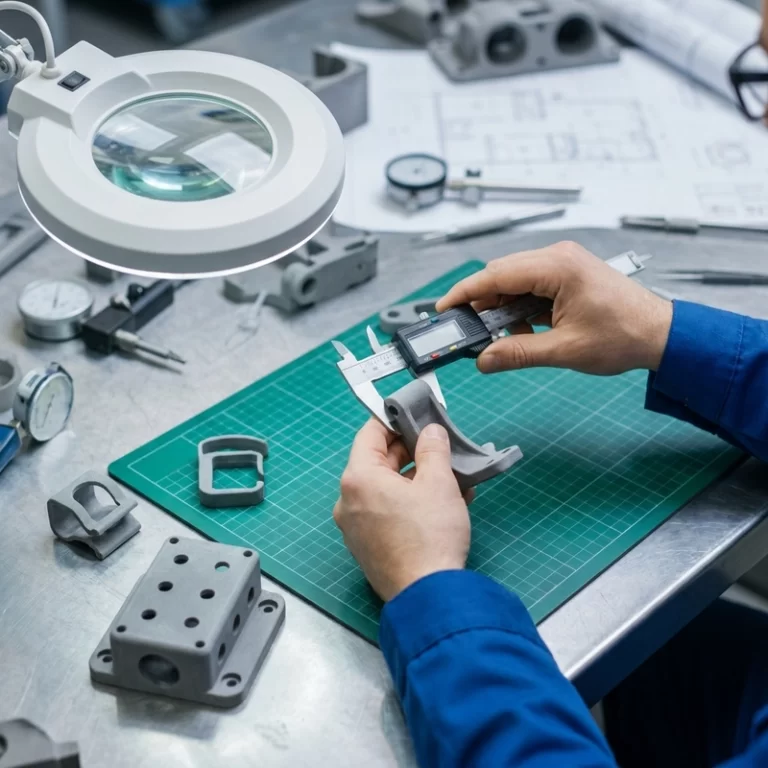
PA12S nylon 3D printing needs a precise material name. One documented commercial example is HP 3D HR PA 12 S enabled by Arkema, an MJF material positioned for surface aesthetics. It is not a generic name for any smoother SLS PA12 part. Confirm which powder and printer system the quote specifies before comparing appearance or performance.
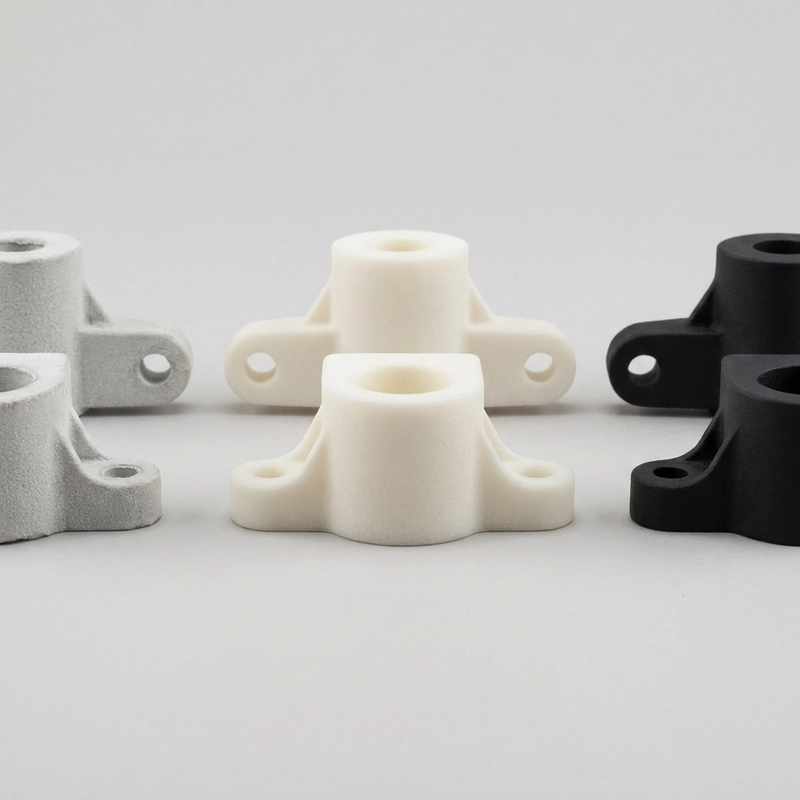
The useful way to think about PA12S nylon 3D printing is this: it may be a better powder-bed choice when the customer cares about appearance, hand feel, and small feature clarity, but still wants nylon-like handling. It is not the answer when the expected surface is glossy injection molded plastic without finishing.
PA12S nylon 3D printing surface quality
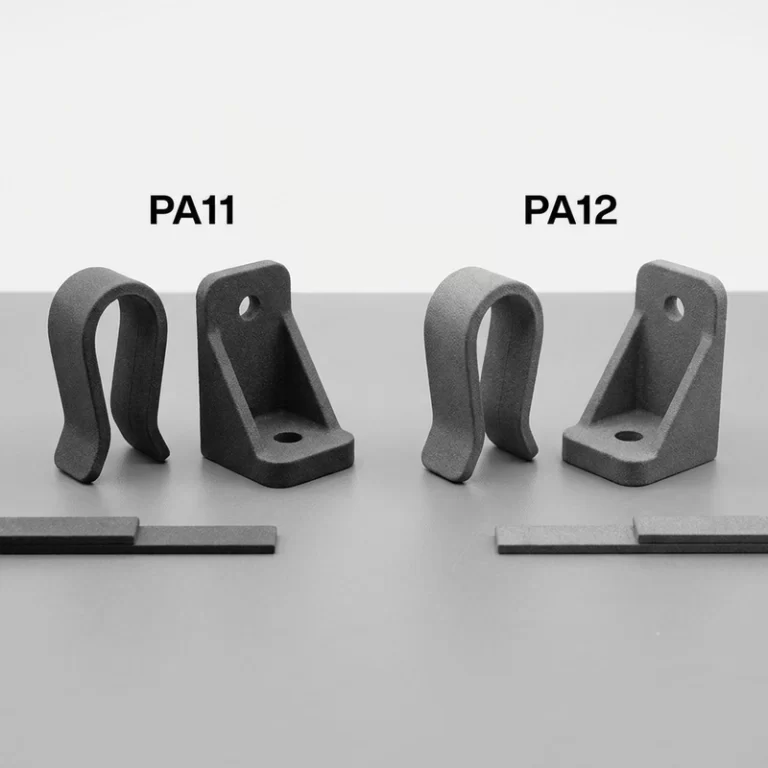
For the HP/Arkema material, HP describes improved surface aesthetics within its specified MJF system. That does not establish one roughness value for every face or finish. Compare physical samples of the proposed material and the alternative under the same finishing and measurement conditions; request the measured faces and method if roughness is an acceptance requirement.
Surface quality still depends on part orientation, build location, powder refresh, blasting, tumbling, dyeing, sealing, and inspection. Down-facing surfaces may look different from side walls. Small holes may hold powder. Thin edges may feel sharper or rougher than broad faces. A smoother material does not remove the need to mark cosmetic faces in the RFQ.
I also separate hand feel from measured roughness. A PA12S sample may feel smoother on a broad face, yet a small slot, underside, or lattice edge can still feel powdery. If the buyer will handle the part often, ask for the same finish on a real geometry, not only a flat sample plaque.
For standard powder-bed finishing choices, Zesmir’s SLS nylon surface finishing article gives more detail on dyeing, tumbling, sealing, and coating.
Accuracy and design limits in PA12S nylon 3D printing
Accuracy, shrinkage compensation and minimum wall thickness belong to the proposed material–machine process and the part geometry. Mark long walls, small clips, thin ribs and critical datums for review. A wall that prints successfully may still distort during cooling or fail during cleanup, finishing or assembly, so the quote needs more than one generic wall or tolerance number.
Holes, clips, and mating surfaces should be designed with powder removal and finishing in mind. A printed hinge or snap feature can work, but the clearance must account for powder-bed texture and post-processing. If the part has critical datums, leave machining allowance or define which surfaces must be checked. PA12S can improve the raw surface, not remove tolerance planning.
Small embossed text and thin decorative ribs need special care. PA12S may show them more cleanly than a rougher nylon powder, but blasting and dyeing can soften edges. If the part needs a serial number, logo, or alignment arrow, make it large enough to survive the full process, not just the CAD preview.
The design rules connect directly to the SLS nylon 3D printing guide and to SLS nylon dimensional accuracy. I would review those before approving a small functional assembly in PA12S.
PA12S nylon 3D printing for appearance parts
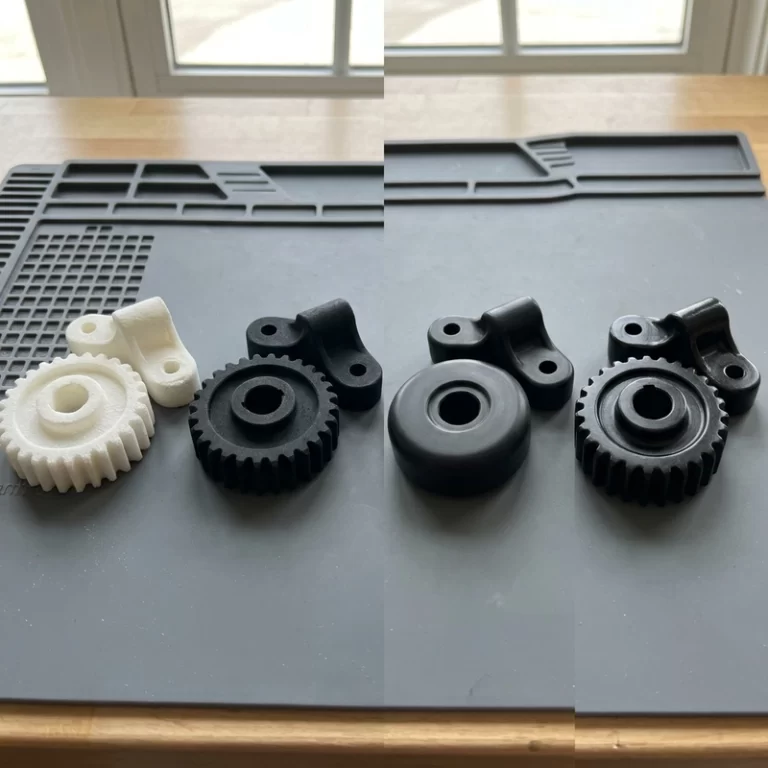
Confirm the raw color of the proposed material and the delivered finish. Dyeing, sealing or painting can change the appearance and feel; each route needs its own approval. If brand color matters, use an agreed color reference and a physical sample instead of assuming that a smoother base material will reproduce the target color.
Appearance parts also need packing control. A smoother surface can still scuff if parts rub together during shipping. For gift samples, consumer prototypes, or display models, I would specify individual wrapping or tray separation. Surface quality is not finished when the part leaves the machine.
PA12S also has a cost question. If the part is a hidden fixture, standard PA12 may be the smarter choice. If the part is handled by customers, used in a presentation, or shipped as a finished sample, the improved surface may justify the extra control. The decision should come from use, not from chasing the newest material name.
I also ask whether the customer really wants PA12S or simply wants a nicer PA12 part. Sometimes standard PA12 with better tumbling, dyeing, or sealing is enough. Sometimes the base surface must improve before finishing can do its job. Comparing one standard PA12 sample and one PA12S sample with the same finish is the cleanest way to decide.
ISO/ASTM 52900 defines additive-manufacturing terminology, not the properties or availability of a commercial PA12 S grade. Use the named material’s documentation for performance comparisons and keep MJF and SLS process labels separate from the polymer designation.
When PA12S is worth considering
- Powder-bed nylon parts where surface appearance matters more than with a shop fixture.
- Consumer product prototypes that need better hand feel than standard PA12.
- Small batches where dyeing or sealing will be used after printing.
- Models that need nylon toughness but cannot look too grainy.
PA12S nylon 3D printing is a useful option when smoother powder-bed nylon is the goal. It should still be quoted with wall thickness, tolerance, finish, color, and handling requirements. Without those details, the word “smooth” becomes too easy to misunderstand.
For RFQ files, include the visible faces, acceptable texture, target color, small lettering, packing needs, and whether the part is appearance-only or lightly functional. PA12S nylon 3D printing works best when “better surface” is tied to a real acceptance sample.