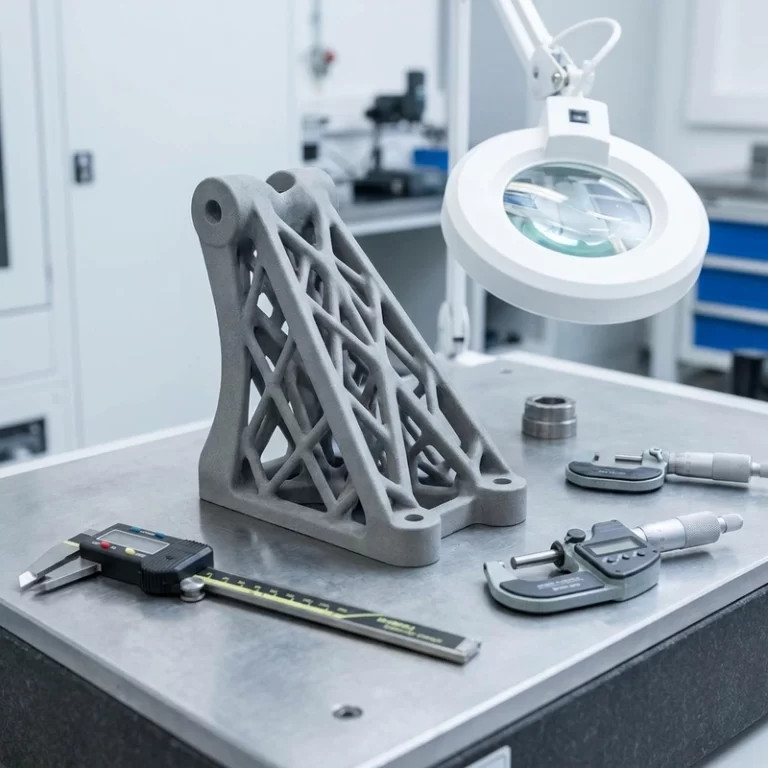
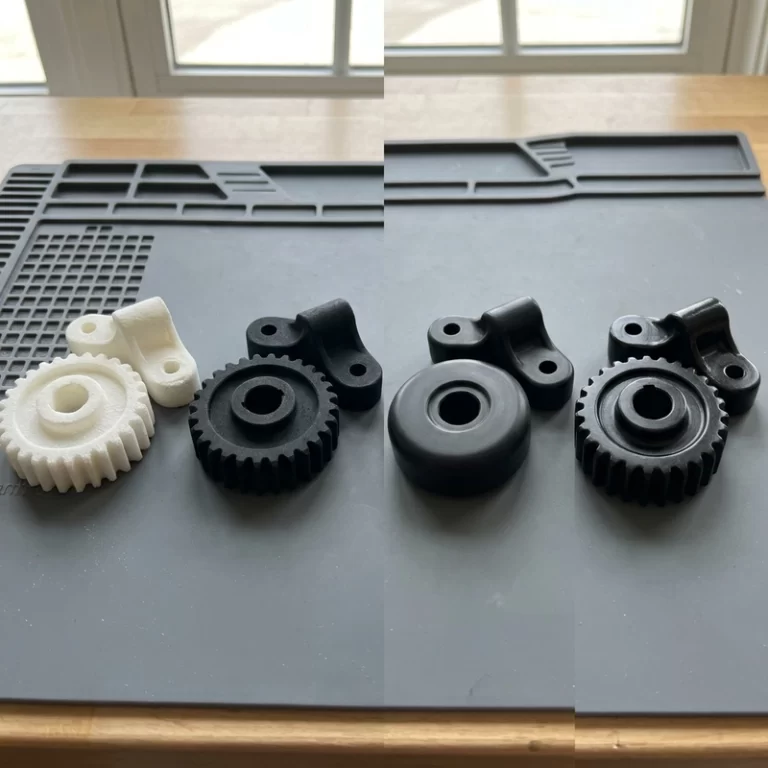
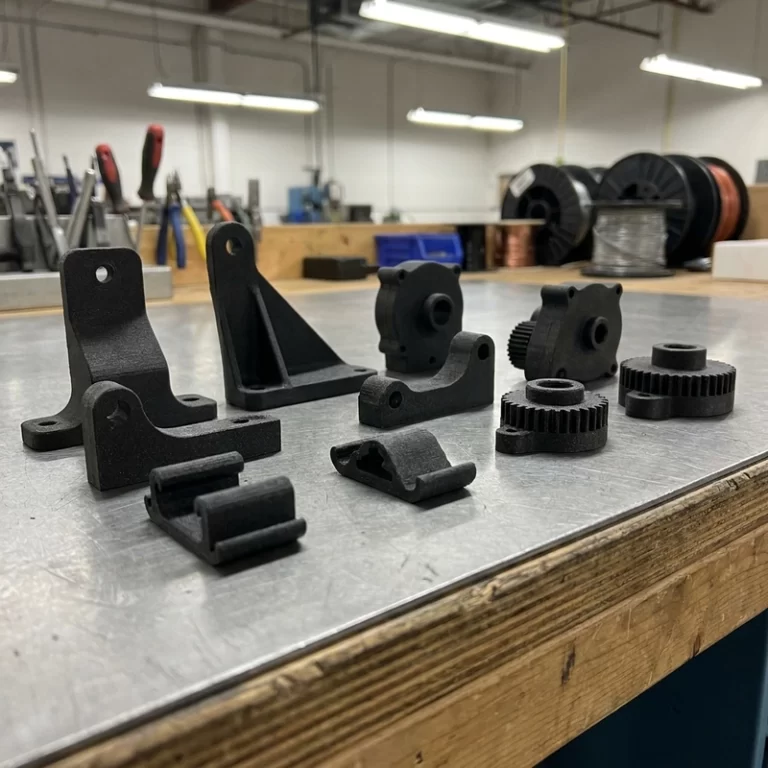
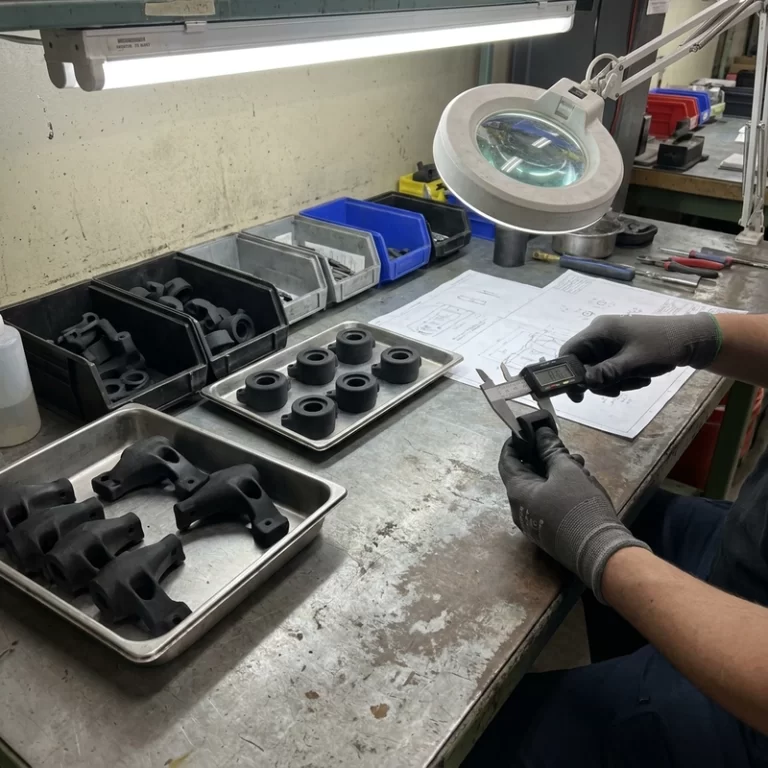
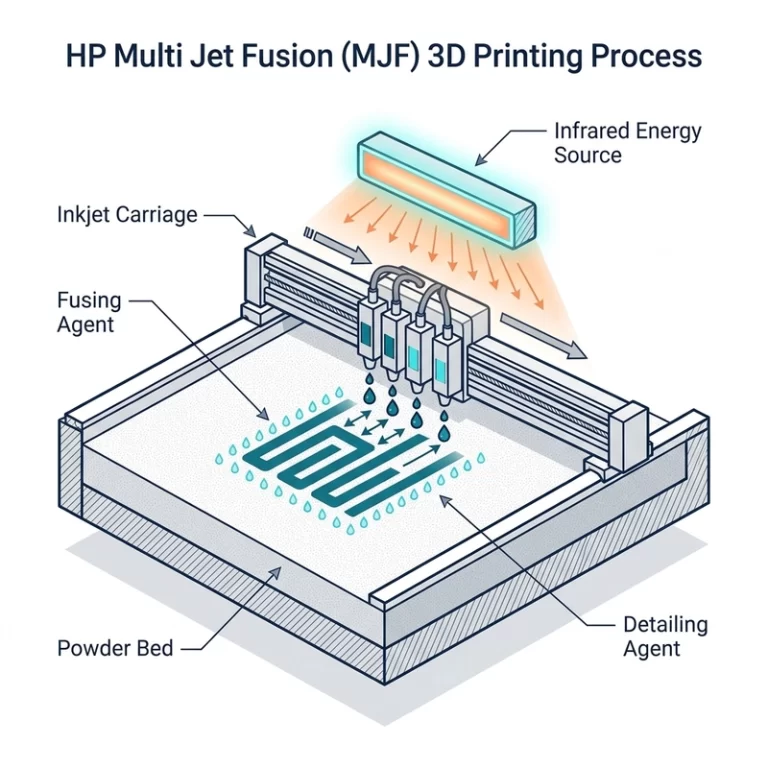
MJF nylon 3D printing builds parts by spreading polymer powder, selectively applying fusing and detailing agents, and using heat to form each layer. The surrounding powder supports the geometry. The finished build still needs controlled cooling, powder removal and the agreed surface treatment before the parts are ready for assembly or review.
For a buyer comparing MJF with SLS, the useful comparison is the delivered part, not just the build price. A bracket may work with a cleaned raw surface; a handheld housing may need a different finish. Holes, clips, channels and repeat-batch requirements should be identified before either route is quoted.
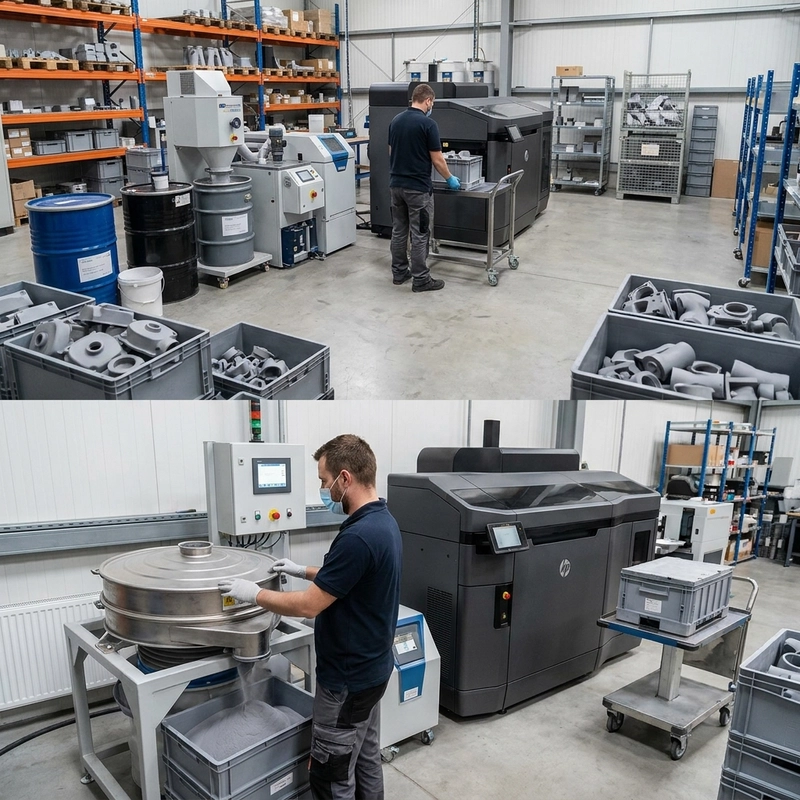
Powder-handling workflow illustration; not a record of a specific production batch.
How MJF 3D Printing Works in a Real Part Workflow
- Prepare the build. Review the material, orientation, spacing and access needed to remove powder from the geometry.
- Form successive layers. Spread powder, apply the agents and use heat to fuse the selected regions. Repeat to build the part.
- Cool and unpack. Allow the build to cool under the process conditions, then extract the parts and recover surrounding powder.
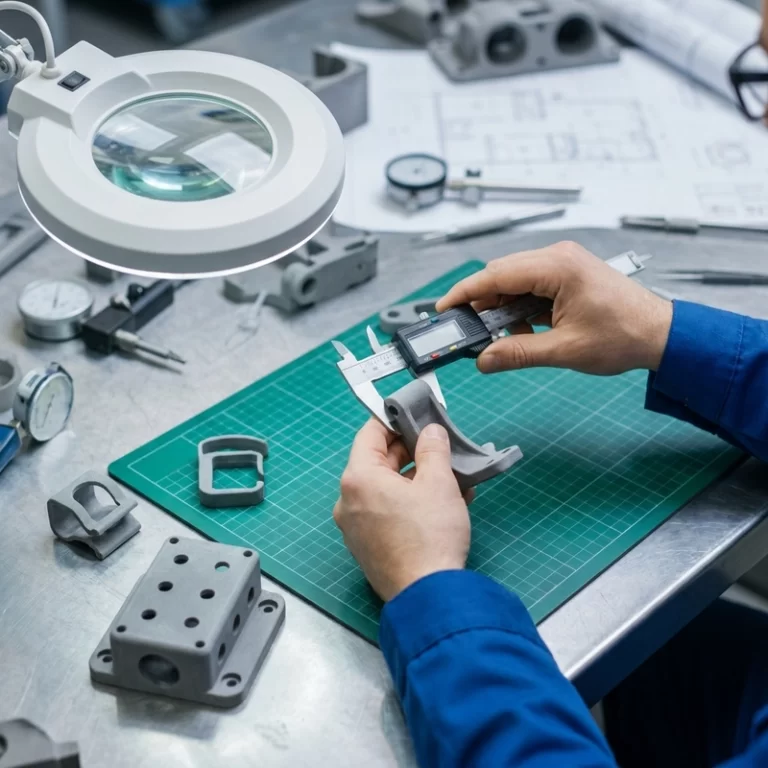
- Clean, finish and check. Remove residual powder, carry out the specified finishing or secondary operations, and check the features that control fit.
SLS instead uses a laser to fuse the selected powder regions. HP’s MJF and SLS process overview explains the difference. Both are powder-bed routes; neither process name alone defines the final tolerance, surface or strength of a particular part.
The important difference is not a slogan like “SLS is flexible” or “MJF is faster”. It is how the build handles heat, powder, agent distribution, part spacing, cooling, and post-cleaning. If the part is a thick housing, a small snap-fit latch, a thin duct, or a nested run of hundreds of small parts, those details matter more than the process label.
Before comparing RFQs for SLS and MJF nylon 3D printing, make four areas explicit: material grade, powder refresh control, build layout, and finish expectation. If any one of those is vague, the first sample may still look acceptable, but repeat production becomes harder to trust.
Powder refresh is not just a cost trick
After a powder-bed build, only part of the powder becomes solid parts. The surrounding powder supports the geometry during printing, then it is recovered during depowdering. Some recovered powder can be screened and blended back with virgin powder. That is normal practice. The problem starts when “reused powder” is treated as if it has exactly the same behavior as new powder.
Powder that has sat through a build has seen heat. It may also have absorbed moisture during storage or handling. Flowability, color, particle condition, and sintering behavior can change. A powder refresh ratio from a forum post is not a universal process specification. The correct blend depends on the material supplier, machine process, part requirement, and whether the batch is a rough fixture or a cosmetic product component.
A practical check is simple: ask whether the refresh ratio is controlled for repeat batches, and whether aged powder is screened, dried, and kept away from critical jobs when needed. For SLS and MJF nylon 3D printing, if the answer is only “we reuse powder to reduce cost”, that is not enough for functional nylon parts. It does not mean the supplier is bad. It means the quote is missing a quality-control detail.
Moisture control matters before the powder reaches the bed
Nylon absorbs water. That is true for filament, pellets, and powder. Excess moisture can contribute to bubbles, rough surfaces, weak areas, and dimensional drift. The exact drying condition should follow the material supplier’s datasheet, not a guessed temperature from another nylon grade.
This is why I link moisture control with powder refresh. A clean refresh plan still fails if storage is sloppy. For a deeper material-side check, pair this article with Zesmir’s notes on nylon 3D printing moisture control and PA12 nylon 3D printing. The buyer does not need to become a powder chemist, but the buyer should know what to ask before approving repeat work.
Nesting changes the batch, not only the invoice
One reason SLS and MJF can be cost-effective is nesting. Many parts share one build volume, and no separate support structure has to be printed and removed in the same way as resin or FDM. That is a real advantage for small-batch production.
Still, maximum packing is not automatically the best build. Thick sections hold heat differently from thin ribs. Large flat faces can behave differently from small clips. In SLS and MJF nylon 3D printing, a batch that mixes heavy housings with delicate snap features may cool unevenly. The result can be slight warping, surface variation, loose hole size, or one corner of the build looking different from another.
The nesting plan should respect part size, wall thickness, heat distribution, and depowdering access. If hollow parts or lattice structures are included, escape holes cannot be an afterthought. Powder trapped inside a closed cavity is not a small cosmetic issue if the part is going into a product, a fixture, or a moving assembly.
| Control point | What can go wrong | What I would ask before approval |
|---|---|---|
| Powder refresh | Rougher texture, color variation, weaker or less repeatable parts | Is the refresh ratio recorded for repeat batches? |
| Powder storage | Moisture-related defects, poor flow, unstable finish | How is PA powder dried and sealed before use? |
| Nesting density | Uneven heating, distortion, mixed surface appearance | Will thick and thin parts be built together? |
| Depowdering | Powder left inside channels, blind holes, lattice areas | Are escape holes and cleaning access designed into the model? |
| Finish route | Raw texture does not match buyer expectation | Is the quote raw, dyed, tumbled, sealed, painted, or machined? |
SLS and MJF nylon 3D printing surface checks
Raw nylon from SLS and MJF usually has a fine powdery texture. That texture is normal. It is also easy to misunderstand. A fixture, robotic bracket, duct, or hidden housing may not need more than depowdering and bead blasting. A handheld product part may need dyeing, tumbling, sealing, coating, or local machining. A gift sample with a logo may need a different inspection plan again.
Do not approve a cosmetic nylon batch from photos alone if the surface matters. Photos can hide powder texture, edge softness and small color shifts. A physical finish sample is often a better control. For visible surfaces, compare the same geometry and finish route rather than assuming that a process name defines the appearance.
Threads, holes, bearing seats, sealing faces, and press-fit zones need separate attention. Printing may create the general shape, but the final function may require tapping, threaded inserts, drilling, reaming, or CNC cleanup. Mark those features in the STEP file or a supporting drawing so the review distinguishes cosmetic openings from holes that must assemble with hardware.
SLS and MJF nylon 3D printing is not a mold texture replacement
This is a common expectation problem. Nylon powder-bed parts can be strong and useful, but the raw surface is not the same as injection molding. If the buyer wants a molded-looking outer shell, the quote should include finishing work or a different manufacturing route. If the buyer wants functional low-volume parts, raw or dyed nylon may be the practical choice.
Preparing an RFQ for repeat nylon batches
The best RFQ is not long. It is specific. Send STEP when geometry and dimensions matter, STL when the mesh is all you have, and mark any areas that must fit with screws, shafts, clips, seals, or other printed parts. Add the target material, quantity, color, finish, and whether the first order is a prototype, a fixture, a sales sample, or a repeat production batch.
For process comparison, keep the exact material and delivered finish consistent between the quotations. For basic powder-bed terminology, the NIST additive manufacturing resource is a neutral external reference. It is useful for vocabulary, not a replacement for checking the actual material datasheet and supplier process notes.
The decision follows the sample’s purpose: if SLS and MJF nylon 3D printing is being used for a one-off visual model, surface expectation matters most. If it is being used for a repeat functional batch, powder refresh, drying, nesting, depowdering, and inspection matter more than the cheapest line item on the quote.
For a manual MJF quotation review, send the model, quantity, intended use, required finish and marked assembly features. Zesmir’s MJF PA12 route can be reviewed against those requirements; confirm the proposed material specification and any extra finishing or inspection in the quotation.