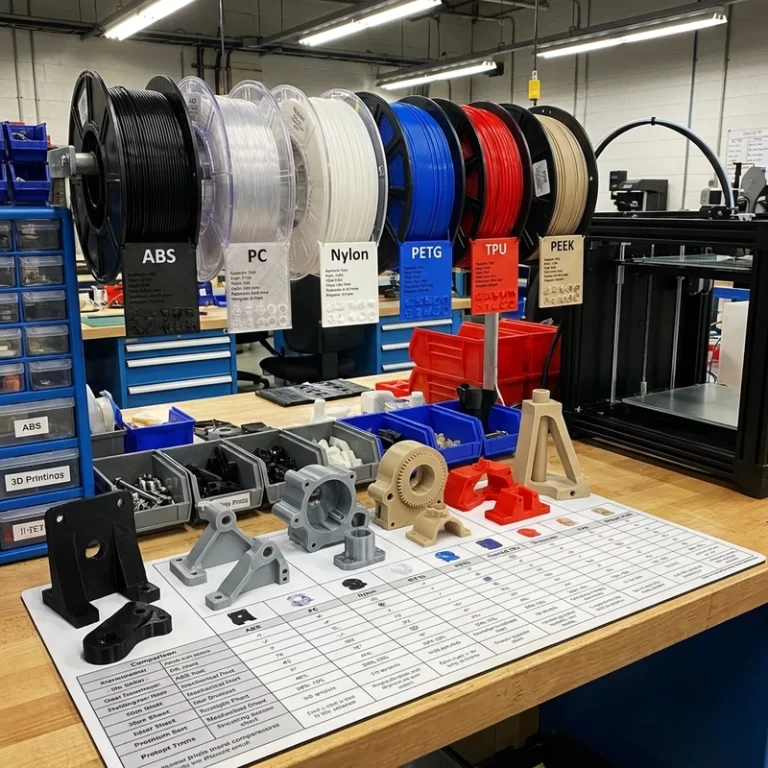
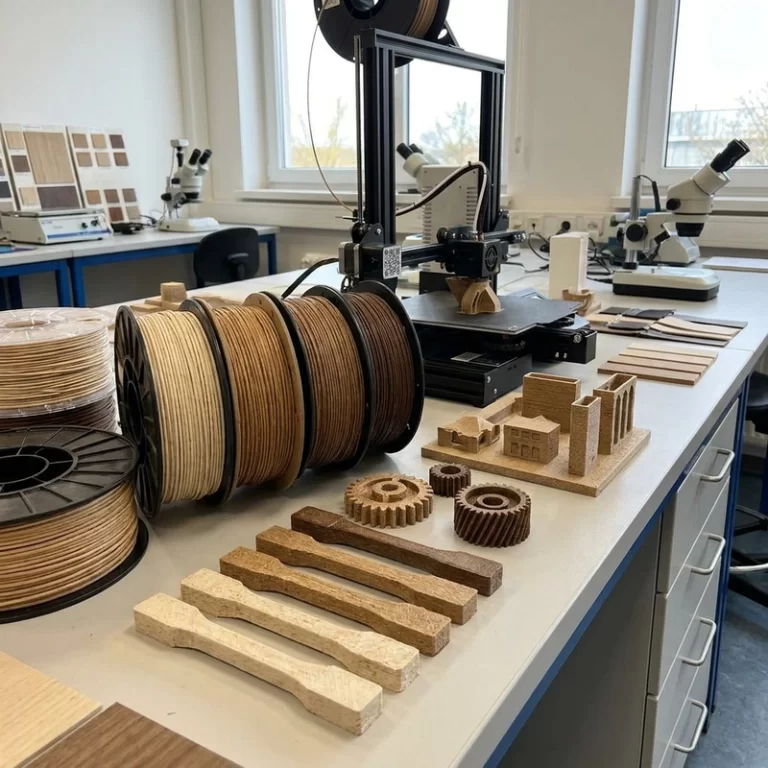
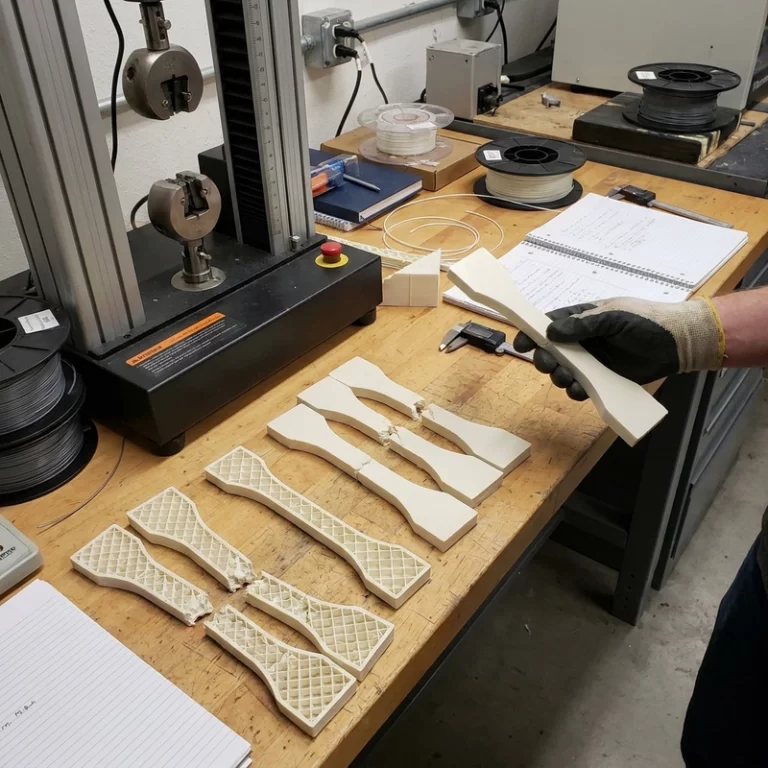
Flexible 3D printing is awkward because soft material starts misbehaving before it reaches the nozzle. TPU, PEBA, and silicone-like systems can stretch, buckle, recover, string, or collapse. A profile that works for PLA can turn into under-extrusion and rounded corners when the filament is soft.
I do not tune flexible parts by temperature alone. The whole path matters: spool condition, drying, extruder grip, unsupported filament length, nozzle size, speed, retraction, support removal, and the way the part relaxes after printing.
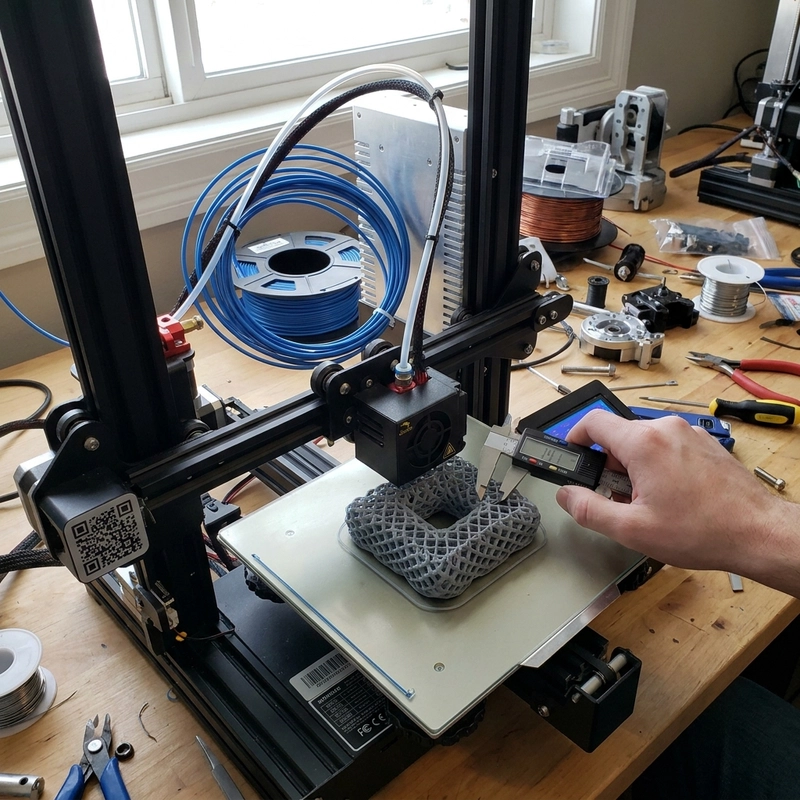
Flexible 3D printing depends on hardness first
TPU is often described by Shore A hardness. Lower numbers such as A60 are softer and more elastic. They can stretch in the extruder and deform at corners. Harder TPU around A90-A95 feeds more predictably, but it still needs enough heat and controlled cooling for layer bonding. PEBA can be light and flexible, but it also needs conservative process control when dimensional recovery matters.
True silicone printing and silicone-like resin printing must be separated. Some silicone systems extrude a paste or liquid and then cure it, so rheology, pressure, nozzle and curing behavior matter. A silicone-like photopolymer is a different chemistry and process. A soft feel alone does not establish silicone composition, sealing performance or long-term behavior.
Speed and retraction are the trap in flexible 3D printing
Softer TPU is more difficult to feed without buckling, so the filament path, drive pressure and supported material profile matter. Use the nozzle temperature and flow limits for the actual grade and extruder. Reducing speed may improve feeding, but hardness alone does not define a transferable temperature or speed window.
Retraction needs restraint. Too little can leave strings, while too much can stretch soft filament, delay extrusion or disrupt feeding. Bowden and direct-drive extruders behave differently. Start from the supported profile for that filament path and tune travel and retraction on a small test instead of assuming one distance and speed will suit all TPU.
| Material behavior | Typical risk | Practical control |
|---|---|---|
| Low Shore TPU | Buckling, corner rounding, feed slip | Low speed and short constrained path |
| Harder TPU | Stringing or weak bonding | Temperature and retraction tuning |
| PEBA | Elastic recovery and size drift | Measure after relaxation |
| Silicone-like paste | Bead collapse or slow cure | Pressure, nozzle, and curing control |
| Wet flexible filament | Bubbles, rough surface, unstable flow | Drying and sealed storage |
Moisture, support, and recovery decide final accuracy
Many flexible materials are moisture-sensitive. Wet TPU can hiss, bubble, string, and leave rough surfaces. Drying instructions must come from the material supplier, but the workflow is straightforward: dry before printing, keep the spool in low humidity, and do not treat a wet-material print as a tuning failure.
Supports are also harder to remove from soft parts. Removal can stretch or tear the model, and a soluble interface helps only when the materials and process are compatible. Measure flexible parts after the specified cooling, curing and conditioning stages. For holes, seals, rings and gripper fingers, check the final unloaded dimensions and the shape under the intended load; a generic shrinkage allowance is not enough.
Flexible 3D printing RFQ notes I want to see
Send the target hardness, material preference, working temperature, whether the part seals, bends, cushions, or grips, and the allowed tolerance after recovery. If it is a gasket, include compression requirements. If it assembles with rigid parts, mark the mating faces. The articles on 3D printed part strength and 3D printing accuracy parameters help separate stiffness, recovery, and measurement issues.
For a neutral standards starting point, ASTM’s additive manufacturing standards overview is useful. On the bench, my rule is more direct: flexible 3D printing succeeds when the process respects softness all the way from feed path to final measurement.
The first sample should be tested the way the part will live. A gasket should be compressed, released, and checked for sealing behavior. A gripper finger should touch the real part it will handle. A wearable pad should be bent and cleaned, not only measured with calipers. Soft materials can pass a dimension check and still feel wrong, recover slowly, or creep under load.
I also avoid approving flexible 3D printing from a part measured straight off the build plate. Let it cool, relax, and finish curing or drying if the process needs it. Then measure holes, lips, sealing ribs, and mating faces. For soft parts, final function is usually more important than a beautiful first measurement.
For color and surface finish, I keep expectations modest until a sample is in hand. Flexible materials often show seams, stringing, and small surface drag marks more clearly than rigid plastics because the bead can stay elastic. If the part is customer-facing, the finish target may change the hardness, support strategy, or even the process route.
I also ask how the part will be stored after delivery. Soft polymers can deform if packed under compression for too long, so packaging is part of approval.