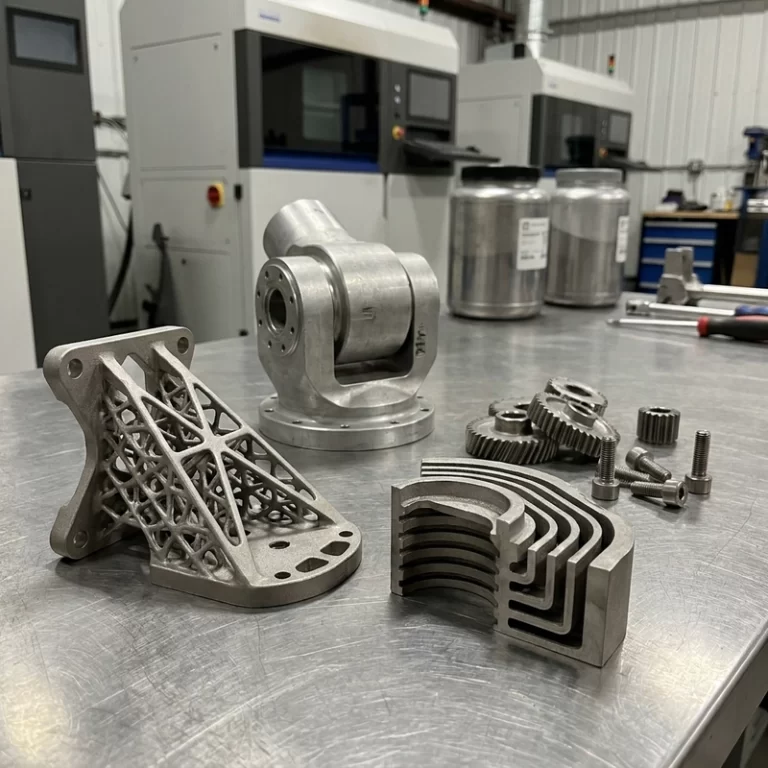
Metal 3D printing powder quality is one of the easiest problems for buyers to miss because the powder disappears inside the supplier’s process. But when a metal print shows porosity, poor surface texture, weak density, color changes, or batch drift, powder condition is one of the first places I look.
Powder is not just “material”. It is a process input with particle size, shape, moisture, oxygen level, contamination risk, reuse history, and storage history. A low quote can be perfectly reasonable, or it can hide aggressive reuse and weak screening. The part drawing alone will not tell you which one is happening.
Metal 3D printing powder quality starts with particle behavior
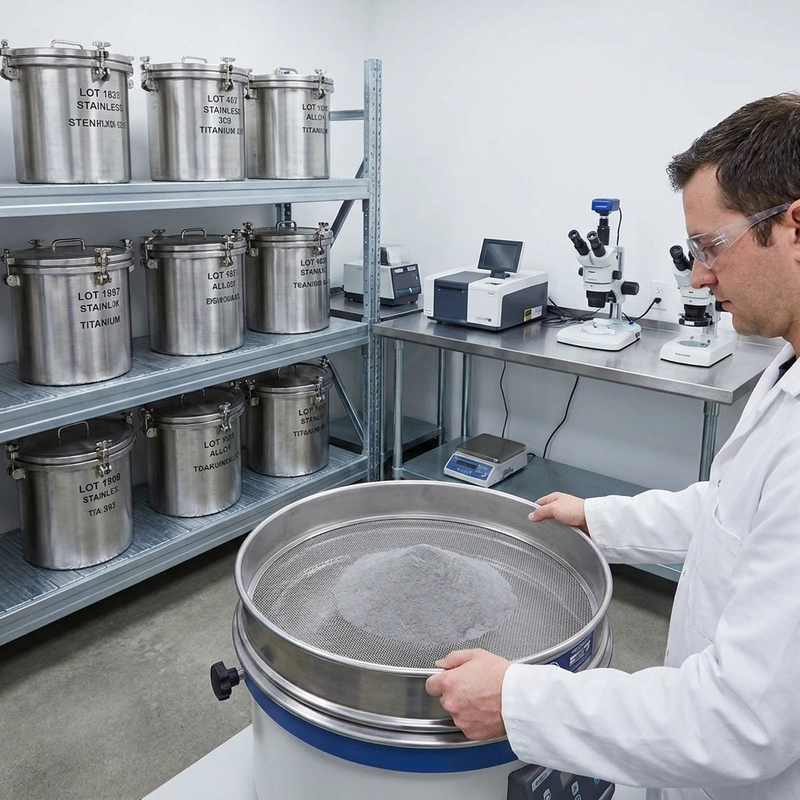
Laser powder bed fusion uses powder with a controlled particle-size distribution, morphology and chemistry. The accepted size distribution must match the machine, alloy and supplier specification. Oversized particles can disrupt thin layers, while an excessive fine fraction can affect flow and handling risk. Irregular particles and satellites can make spreading inconsistent. Review the powder certificate and the actual spreading behavior rather than accepting one nominal size range for every LPBF system.
Good powder should spread into a smooth layer. Bad powder can leave streaks, gaps, or thick spots. Those layer defects may become lack-of-fusion pores, rough surfaces, or dimensional variation. The defect article on SLM metal 3D printing defects connects those symptoms to the printed part.
Moisture, oxygen, and contamination change the risk
Moisture can become gas during melting. Oxygen can form oxide films and embrittle sensitive alloys. Contamination from mixed powders, dirty handling tools, or poor chamber cleaning can create defects that are hard to diagnose after the part is built.
Titanium powder requires particular care in storage, handling and atmosphere control. Use the powder supplier’s safety data sheet and the machine’s approved handling procedure; do not improvise an oven-drying cycle for reactive metal powder. Any drying or conditioning process and chamber oxygen limit must be specified for the powder and equipment. The titanium article on TC4 titanium SLM 3D printing explains why atmosphere records matter.
Metal 3D printing powder quality changes after reuse
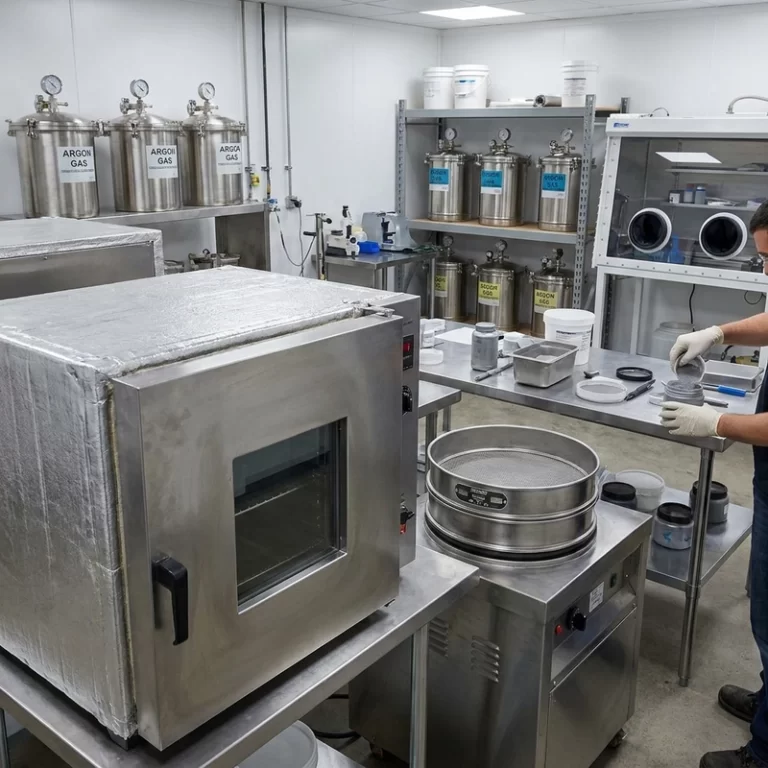
Recovered powder can often be reused after screening and blending, but it is not automatically the same as virgin powder. Heat exposure, spatter, fines, oxygen pickup, and handling all change the material pool. I want a reuse rule, not a vague “we recycle powder”.
Screening removes oversized particles and spatter. Blending controls consistency. Storage protects against humidity and contamination. The related note on metal powder preprocessing goes deeper into that shop-floor step.
What I expect in a metal powder record
For simple visual metal samples, a short process note may be enough. For functional parts, I expect more. Powder lot, supplier specification, drying condition, sieve step, reuse count, blend rule, storage condition, and chamber atmosphere records all help explain why one batch matches another.
The record does not need to be fancy. It needs to be usable when something changes. If a later batch shows more porosity, the shop should be able to check whether powder age, reuse ratio, oxygen, or screening changed. Without that trail, troubleshooting becomes guessing.
I also separate powder cost from finished-part cost. Cheap powder handling can create expensive inspection failures, reprints, or machining scrap. Metal 3D printing powder quality is a cost issue because it affects how many parts survive the whole route, not because powder price alone decides the quote.
Bad powder control does not always leave one obvious signature. It can look like random pores in one area, a rough patch near an overhang, a layer streak that becomes a weak band, or a surface that machines differently from the previous batch. That is why I avoid changing five machine settings before checking powder history.
For binder jetting, powder packing and sintering behavior are just as important, even though there is no melt pool during printing. For SLM, spreading and laser interaction are more visible. In both cases, metal 3D printing powder quality becomes part of dimensional accuracy, density, finish, and repeatability.
One practical RFQ line is enough to start: “Please state whether virgin or reused powder will be used, and how reused powder is screened and blended.” The answer may be short, but it tells you whether the supplier treats powder as controlled material or shop background.
For repeat production, I would add one more request: keep the powder route consistent between sample and batch, or tell me what changes. Metal 3D printing powder quality is hard to evaluate if the approved sample used one powder condition and the batch quietly uses another.
| Powder factor | What it can affect | Question to ask |
|---|---|---|
| Particle size | Layer uniformity and surface finish | What range is specified? |
| Moisture | Gas pores and spatter | How is powder dried? |
| Oxygen | Ductility and oxidation risk | Is oxygen tracked? |
| Reuse | Batch consistency | What reuse rule is used? |
| Contamination | Unexpected defects | How are tools and storage separated? |
NIST additive manufacturing is useful for broader process context. In an RFQ, keep it practical: ask how metal 3D printing powder quality is controlled for the alloy, whether reused powder is screened and recorded, and what inspection is used when the part is more than a visual sample.