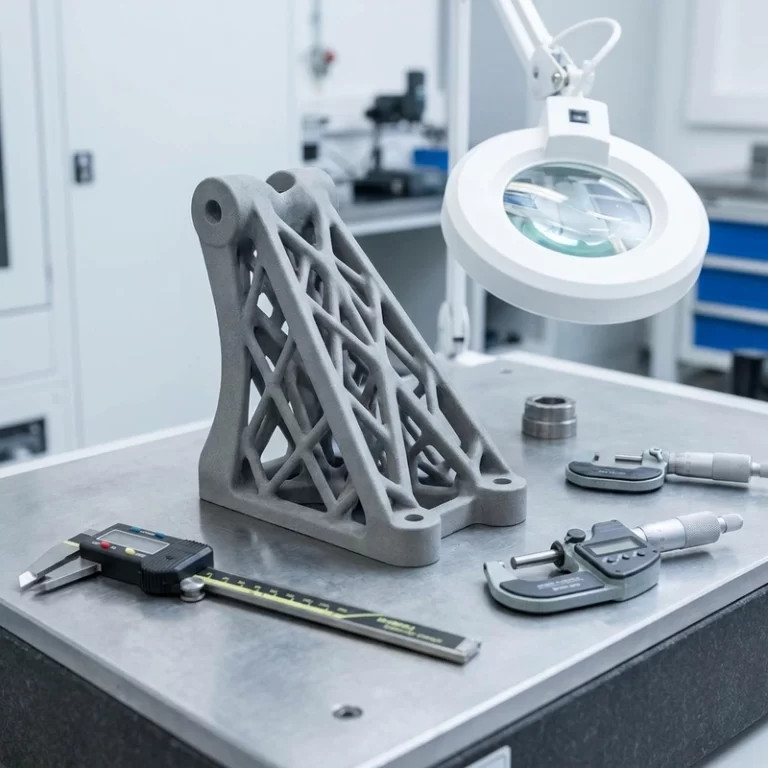
Food-safe nylon 3D printing is not a label I would accept from the material name alone. Nylon may be a familiar engineering plastic, but food-contact use depends on the exact material, additives, powder or filament handling, printer cleanliness, post-processing, migration testing, and the intended contact condition. A printed part is not food-safe just because the base polymer sounds acceptable.
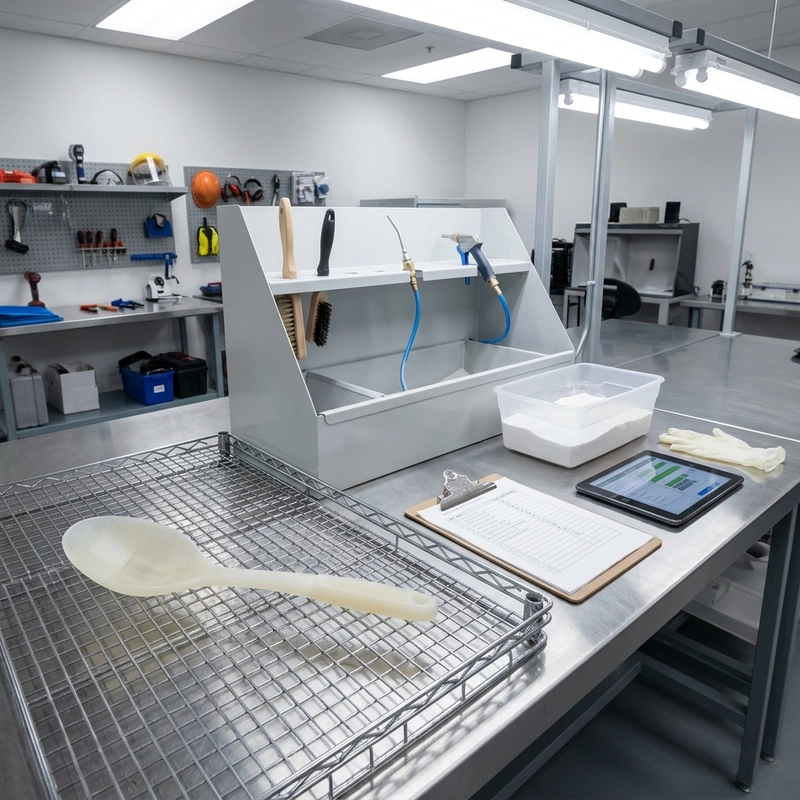
I write this carefully because overclaiming food safety is a real risk. A prototype spoon, coffee-machine part, food fixture, or packaging-contact sample may look harmless, but the print surface can hold powder, pigment, cleaning residue, dye, coating, or trapped contamination. Food-safe nylon 3D printing should be treated as a controlled manufacturing route, not a casual material choice.
Food-safe nylon 3D printing starts with certification scope
Identify the destination market, exact intended use and applicable current requirements with the responsible compliance specialist. A supplier statement, a material authorization and evidence for the finished printed article answer different questions. Do not infer compliance from a generic nylon name or a migration limit quoted without its applicable scope and test conditions.
For US context, consult FDA guidance on determining component regulatory status. It distinguishes substance identity, specifications and permitted conditions of use. An authorization must apply to the actual source and use; a generic “FDA material” claim is insufficient.
If the application is truly food-contact, ask for the exact material grade, colorant, process route, post-treatment, and available test report. Do not ask only whether “nylon is food-safe.” That question is too vague to be useful.
Process cleanliness in food-safe nylon 3D printing
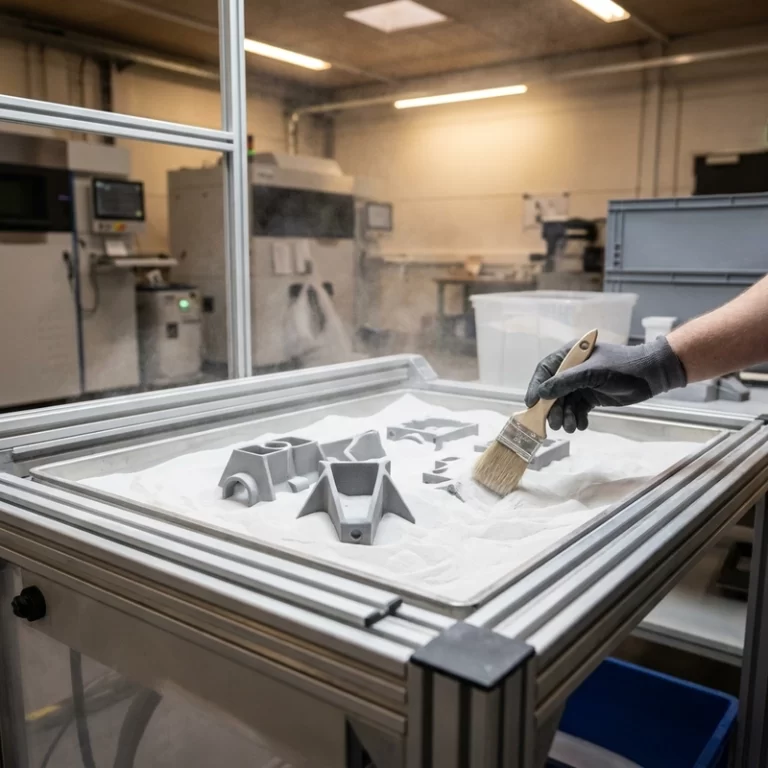
SLS or MJF nylon powder runs through a machine, recoater, powder handling system, sieves, blast cabinet, and finishing area. If the same equipment handles non-food materials, color powder, recycled powder, coatings, or contaminated parts, the process history matters. Cleanliness is not only the final wash. It begins with material storage and machine control.
Printing heat does not establish cleanliness or safety of the completed supply chain. Review depowdering, cleaning, finishing and handling against the actual process and intended contact. Do not select a cleaning pressure or sintering temperature from a general food-safety article.
Powder-bed nylon surfaces are slightly porous and textured. Powder trapped in small holes, channels, and blind pockets is hard to verify. For food-contact design, avoid deep blind cavities, sharp internal corners, and surfaces that cannot be inspected or cleaned. If the geometry cannot be cleaned, the material certificate alone does not solve the problem.
Machine segregation is another question I would ask early. If food-contact work is mixed with ordinary prototype powder, dyed parts, or unknown customer materials, cross-contamination risk becomes difficult to explain later. A serious food-safe nylon 3D printing request should ask how the supplier separates material lots, cleaning tools, blasting media, and packing areas.
Surface finishing and food-safe nylon 3D printing limits
Finishing may change roughness, residues and cleanability. Review the actual abrasive, cleaner or coating and its intended contact conditions. A clear coat or a sanding sequence does not independently qualify an ordinary print for food contact.
Specify food type, contact time and temperature, chemical exposure, washing and reuse conditions. These must fit the exact material and applicable authorization; one temperature threshold cannot establish the safe use limit of every printed nylon article.
For general powder-bed nylon behavior, read Zesmir’s SLS nylon 3D printing guide. For the moisture side of nylon quality, the nylon 3D printing moisture control article is the better companion.
Where food-contact printing may make sense
Food-safe nylon 3D printing may be considered for development fixtures, short-run handling aids, shape prototypes, jigs outside direct food zones, or parts that later go through formal material and migration review. It is a poor fit for vague consumer claims, rough porous surfaces touching wet food, hidden channels that cannot be cleaned, or applications where the buyer cannot define the regulation.
For RFQ work, separate three categories: visual food product prototype, indirect food equipment part, and direct food-contact component. The first may only need appearance. The second may need cleanability and non-contamination controls. The third needs serious documentation and testing. Mixing these categories creates dangerous assumptions.
Repeated washing, heating and abrasion can change the part. Define how it will be cleaned, inspected and replaced, and assess that life cycle under the intended conditions. A display model that does not contact food is a different application from either single-use or repeated-use food-contact equipment.
Traceability matters if the part leaves prototype status. Keep the material lot, print date, post-processing route, cleaning method, and any test document connected to the part. Without traceability, it becomes difficult to explain which process produced a later replacement or repeat batch.
A useful review package identifies the grade, material source, food type, contact conditions, cleaning, colorants or coatings, process and supporting documentation. Do not release the article for food contact while those requirements are unresolved; calling it a prototype does not change its actual intended use.